

Portable Ergonomic On-Site Valve Seat Repair Design
The LD2000 is a portable valve seat boring machine for 16–50 mm seats on cylinder heads that can stay on the engine. Weighing 7 kg, the workhead carries to the vehicle and the magnetic base clamps to the head surface once the valve and spring are removed — no dedicated machining bay, and no loading a head into a truck. The 50–150 RPM variable-speed spindle is standard rather than an add-on, which covers motorcycle singles and twins, passenger car petrol and diesel heads, and light van heads in one machine. Typical users are motorcycle workshops, general repair garages bringing valve work in-house, and mobile engine rebuilders working on site.
Dual Air-Cushion High-Concentricity Precision Machining
Valve seat accuracy depends on one thing: whether the cutter axis is concentric with the valve guide axis. A seat off-centre by 0.05 mm will not seal, however good the cutter is. The LD2000 mounts through a pilot that sits stationary in the guide while the spindle rotates around it — a dead-pilot design that references the cutter to the guide itself. Two spherical air cushions float the boring body until it self-aligns, then lock it in that position, so concentricity comes from the valve guide rather than from the rigidity of a floor-mounted column. Depth reads on a vernier scale in 0.02 mm increments, and the spindle tilts through 8° for canted and compound-angle seats.
Wide Compatibility & Cost-Saving Universal Tooling
Three-angle carbide form tools cut the complete seat profile — 30°, 45° and 60° plus top and bottom chamfers — in a single pass. That is the difference between cutting and grinding: a valve seat grinder works one angle at a time with an abrasive stone and depends on operator feel, while cutting builds the geometry into the tool and repeats it from seat to seat. The LDXY tool series is supplied in three ranges (18–35 mm, 32–45 mm and 35–65 mm), with MM type pilots at 9.52 mm (3/8″) shank in diameters from 3.5 mm to 14 mm. Because this is the same tooling used on the LD180 and LD100 ranges, an existing LD owner shares cutters and pilots.
Solid Rigid Construction for Long-Term Stable Operation
The cast frame and clamped base suppress cutting vibration, which is what lets a 7 kg machine hold repeatability across a run of seats rather than only on the first one. That reliability has a limit worth stating: a floor-type seat and guide machine still wins above roughly ten heads a week, on guide reaming and replacement in the same setup, and on seats wider than 50 mm. Below that, this machine does the seat work alone at a fraction of the cost of a USD 18,000–30,000 floor unit. Shops that run both keep the portable machine for motorcycle and one-off jobs.
Technical Specifications
| Model | Portable Valve Seat Boring Machine |
| Machining capacity | 16 – 50 mm (0.63 – 2″) |
| Sphere-cylinder travel (radius) | 2.5 mm (0.10″) |
| Spindle stroke | 15 mm (0.6″) |
| Spindle rotation speed | 50 – 150 RPM |
| Cutting tools | 18 – 35 mm / 32 – 45 mm / 35 – 65 mm |
| MM type pilot | Φ9.52 mm – 3/8″ shank; Φ3.5 – Φ14 mm 190 mm length |
Customer Experience
Trusted by Automotive Repair Professionals
Real experiences from workshops worldwide
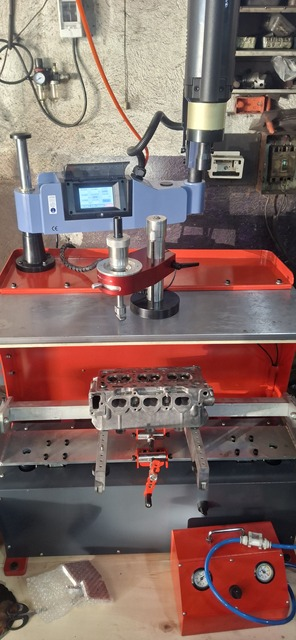
Philippines
Satisfied with LD2000 Performance
“The LD2000 Valve Seat Cutting and Boring Machine is a high-quality and reliable machine for engine cylinder head rebuilding work.”
— Jaime Dizon
Philippines
View More Customer Stories →
FAQ
1 What engine types is the LD2000 valve seat boring machine compatible with?
The LD2000 is compatible with a wide range of engine cylinder heads, including those from passenger cars, light trucks, motorcycles, agricultural equipment, and small industrial engines. Its versatile clamping system and adjustable boring range allow it to accommodate different valve sizes and cylinder head configurations commonly found in automotive and small engine repair workshops.
2 What makes the LD2000 portable and why is that an advantage?
The LD2000’s compact, self-contained design makes it easy to transport between workstations or to on-site repair locations. Unlike large stationary boring machines, the LD2000 does not require a dedicated machining bay. This portability allows mobile engine rebuilders and small workshops to perform professional valve seat machining without heavy infrastructure investment.
3 Can a compact machine like the LD2000 deliver professional-grade machining precision?
Yes. Despite its compact size, the LD2000 is built with a precision-ground spindle, rigid boring bar assembly, and fine-adjustment controls that deliver centering accuracy and concentricity matching or exceeding larger stationary machines. Its design prioritizes the critical alignment between the pilot, cutter, and valve guide, which is the foundation of accurate valve seat machining.
4 Is the LD2000 suitable for small engine repair workshops?
Absolutely. The LD2000 is an ideal entry-level valve seat boring solution for small workshops, motorcycle repair shops, and part-time engine builders. Its affordable price point, minimal space requirements, and straightforward operation make professional valve seat machining accessible to shops that cannot justify a large, expensive dedicated boring station.
5 How cost-effective is the LD2000 compared to outsourcing valve seat work?
The LD2000 is a highly cost-effective investment. Performing valve seat boring in-house eliminates the per-job cost and turnaround delay of sending cylinder heads to a machine shop. For a workshop doing regular valve jobs, the machine can pay for itself within a few months through savings on outsourcing fees and the ability to offer faster, more competitive engine rebuilding services.